1.Hard wear surfaces
Resists abrasion in guides, liners and sliding components; finish and counterface remain important.
Alumina (Al₂O₃) combines hard wear surfaces, electrical insulation and chemical stability for industrial components and electronic substrates. Purity and microstructure distinguish general-purpose and higher-purity grades.
95%, 96%, 99%, 99.5% and 99.7%+ alumina ceramics
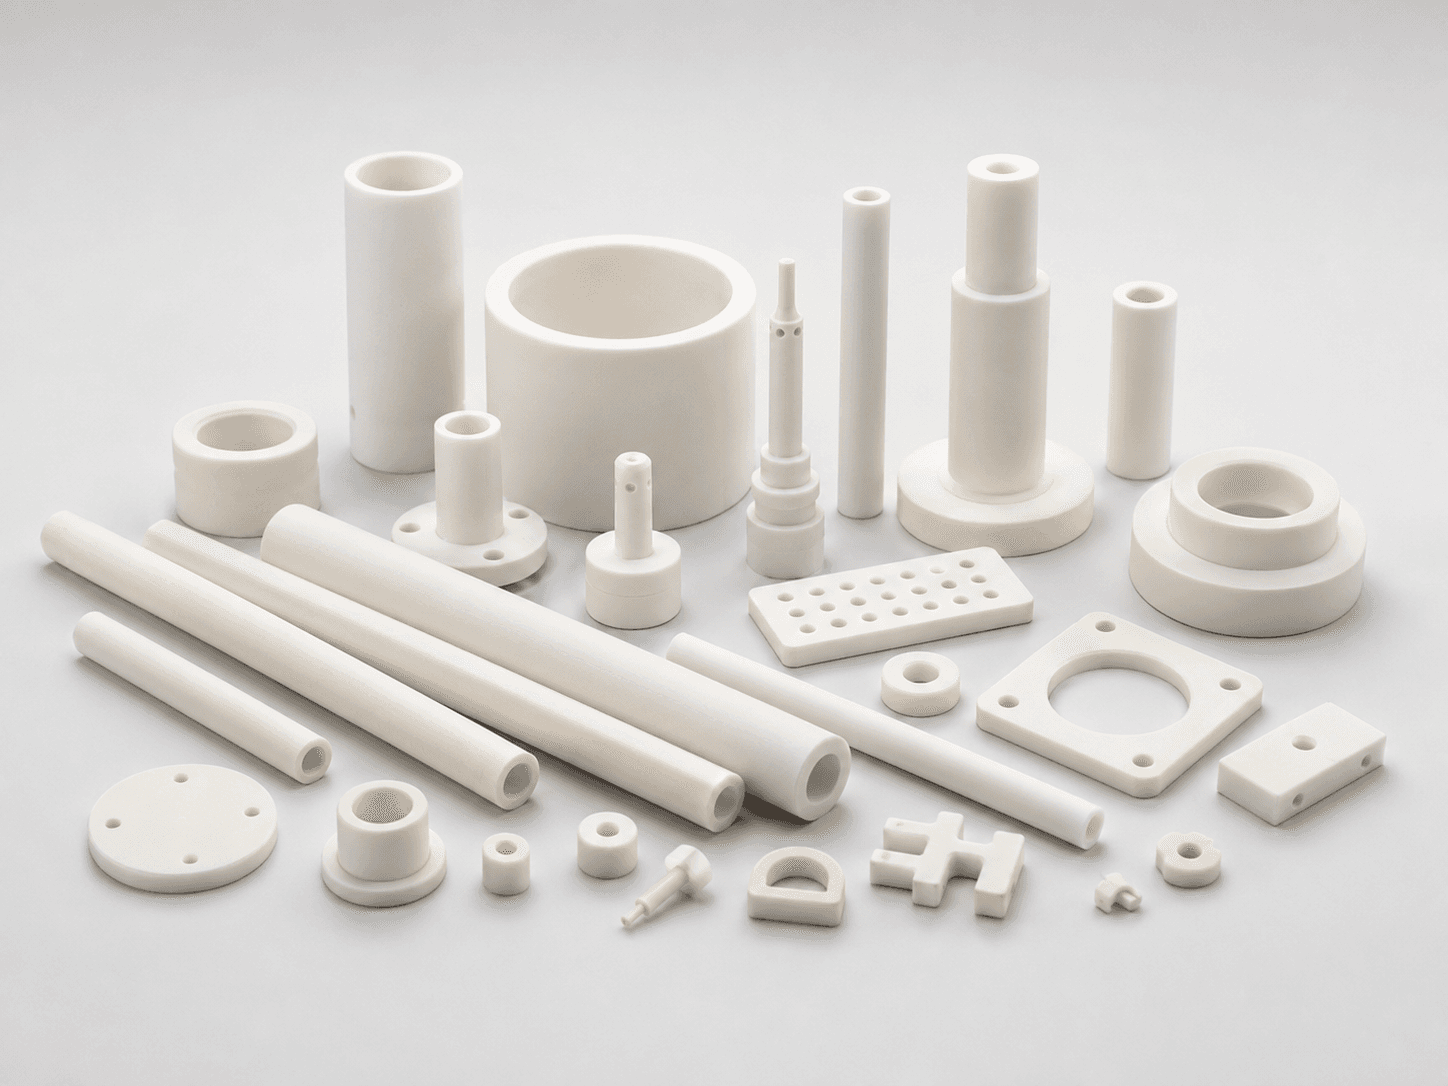
Resists abrasion in guides, liners and sliding components; finish and counterface remain important.
Supports insulating components and substrates. Performance depends on temperature, thickness and electrical loading.
Useful in many process environments; confirm compatibility with the actual medium and concentration.
A candidate for hot-zone supports and protection tubes, with grade-specific limits for load and thermal cycling.
A broad range of purities lets designers balance wear, insulation, cleanliness and component cost.
Bushings, spacers and supports provide electrical separation in compact assemblies.
Insulating substrates provide mechanical support with moderate heat conduction.
Hard contact surfaces address abrasion in handling and processing equipment.
Sealing faces and flow components combine wear resistance with medium-specific chemical compatibility.
Protection tubes and supports serve hot zones when purity, atmosphere and thermal cycling are qualified.
| Material / route | Density (g/cm³) | Bending strength (MPa) | Conductivity (W/(m·K)) | Material distinction |
|---|---|---|---|---|
| 96% alumina | 3.72 g/cm³ | 343 MPa (4-point, 20°C) | 24.7 W/(m·K), 20°C | General-purpose insulation and wear reference. |
| 99.5% alumina | 3.90 g/cm³ | 300 MPa (4-point, 20°C) | 30.0 W/(m·K), 20°C | Higher purity; not automatically higher flexural strength. |
| Sintered Y-TZP zirconia | 6.02 g/cm³ | 1240 MPa (4-point, 20°C) | 2.2 W/(m·K) | Higher strength and lower heat conduction; review hydrothermal ageing. |
| Magnesia-stabilized zirconia | 5.72 g/cm³ | 620 MPa (4-point, 20°C) | 2.2 W/(m·K) | A distinct stabilized zirconia grade, not an alumina substitute by default. |
Form blanks for sintering; geometry and production volume guide the route.
Consider near-net forming for repeatable complex shapes, with tooling and shrinkage allowances.
Evaluate extrusion for consistent sections and tape casting for thin substrate formats.
Finish sintered contact surfaces and critical dimensions to drawing-defined requirements.
Process availability and acceptance criteria are confirmed for the selected component.
Send the drawing, quantity, medium, temperature cycle, load and critical surfaces. Material route and process options are confirmed for the selected part.
Request a quote